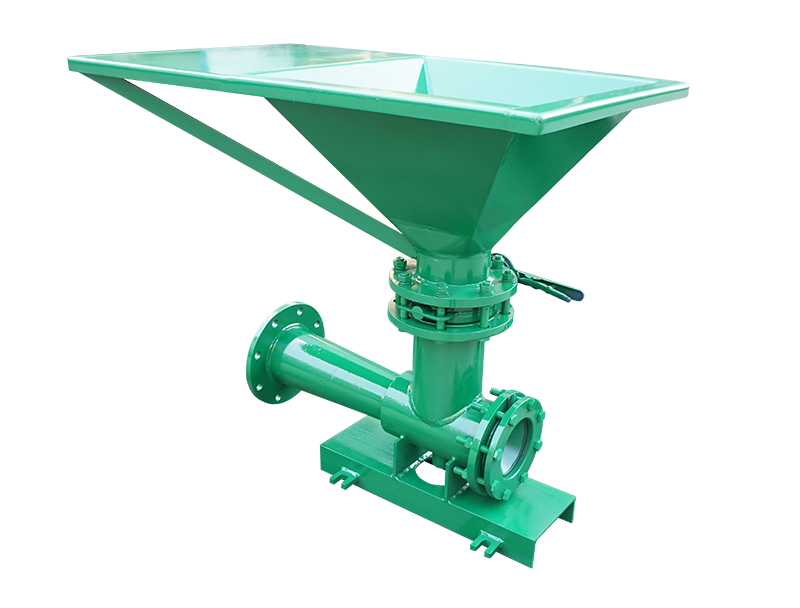
How to Choose the Best Mud Separator for Efficient Drilling Operations
By:Admin
Company News & Blog
High-Quality Drilling Rig Parts and Drill Drilling Rig Drawworks for Reliable Performance
**China's Drilling Rig Parts and Drill Drilling Rig Drawworks: Advancing the Future of Drilling Technology**In recent years, China has solidified its position as a pivotal player in the global drilling industry, driven by rapid industrial development and increasing demand for energy resources. Central to this growth is the evolution and manufacture of critical drilling rig components, including drilling rig parts and drawworks, which serve as the backbone for efficient and safe drilling operations. As the industry continues to innovate, these components are witnessing significant improvements in design, quality, and technology, fostering enhanced performance and reliability for drilling rigs worldwide.---### Modern Drilling Rig Parts: Enhancing Efficiency and DurabilityDrilling rig parts are essential for the smooth operation of any drilling rig, encompassing a wide array of components such as rotary tables, top drives, mud pumps, hoist systems, and safety mechanisms. The quality and precision of these parts have a direct impact on the drilling process's efficiency, safety, and cost-effectiveness.In China, manufacturers have adopted cutting-edge technologies and stringent quality control processes to produce drilling rig parts that meet international standards. Innovations in materials science have led to the use of more durable alloys and composites, which resist wear and corrosion even in the most challenging drilling environments. This not only extends the lifespan of the parts but also reduces maintenance costs and downtime, thereby maximizing operational productivity.Moreover, Chinese drilling rig parts suppliers have emphasized customization to meet specific client needs. Whether for onshore or offshore drilling, shallow or ultra-deep wells, these tailored solutions ensure optimal compatibility and performance. The incorporation of digital monitoring systems within some components allows operators to track real-time data such as temperature, pressure, and mechanical stress, enabling predictive maintenance and enhancing safety protocols.---### Drill Drilling Rig Drawworks: Powering Precision and ControlA critical element in drilling rig operations is the drawworks, a large winch that plays a vital role in raising and lowering the drill string and attached tools into the wellbore. The performance of the drawworks directly affects the ability to maintain well control, manage drill pipe movements smoothly, and respond quickly to emergencies.Chinese manufacturers have made significant strides in the design and manufacture of drill drilling rig drawworks by focusing on power, control, and durability. Modern drawworks systems incorporate advanced hydraulic and electric drive technologies that offer precise speed regulation and torque control. This sophistication enables smoother operation, reduces mechanical shocks, and prevents equipment damage.Furthermore, the integration of automated control systems in drawworks allows for enhanced operational safety. Automated braking systems and emergency shutdown features help mitigate risks in hazardous drilling environments. The adoption of modular designs has also facilitated easier maintenance and component replacement, contributing to reduced downtime and improved operational continuity.The enhanced drawworks manufactured in China are designed to handle a broad spectrum of drilling challenges, from conventional oil and gas wells to complex geothermal and exploration projects. Their increasing reliability and advanced features have garnered international attention and adoption, underscoring China's growing reputation as a leading supplier in the drilling equipment sector.---### Industry Outlook and Future TrendsThe ongoing global energy transition, characterized by a shift toward cleaner and more sustainable resources, is reshaping the drilling industry. To remain competitive, Chinese manufacturers of drilling rig parts and drawworks are investing heavily in research and development to innovate greener and more efficient drilling technologies.One emerging trend is the development of smart drilling rigs equipped with Internet of Things (IoT) sensors and artificial intelligence (AI) systems, enabling real-time data analytics and enhanced decision-making. These smart rigs utilize advanced drilling rig parts and drawworks integrated with intelligent control systems to optimize drilling parameters, minimize environmental impact, and ensure operational safety.Another growth area is the emphasis on environmental compliance and sustainability. Chinese companies are exploring eco-friendly materials and energy-efficient designs for drilling rig components to reduce carbon footprints and meet stricter regulatory standards. Additionally, efforts to improve component recyclability and minimize waste during manufacturing are gaining momentum.---### ConclusionChina’s drilling rig parts and drill drilling rig drawworks have increasingly become synonymous with innovation, reliability, and quality in the global drilling equipment market. Through continuous technological advancement and commitment to international standards, Chinese manufacturers are not only supporting the domestic energy sector but are also contributing to the efficiency and safety of drilling operations worldwide.With a strategic focus on smart technologies, sustainability, and customization, the future of Chinese drilling rig components looks promising. As global energy demands evolve and drilling challenges become more complex, these enhanced parts and drawworks will continue to play a crucial role in powering safe, efficient, and environmentally responsible drilling activities across the globe.
Highly Efficient and Durable 3x4 Centrifugal Pump for Mission Purposes
Mission 3x4 Centrifugal Pump, a Leading Innovation in Water Pump TechnologyIn the world of industrial and agricultural machinery, the name {Company Name} has been synonymous with cutting-edge technology and top-quality products for over two decades. With a strong commitment to innovation and customer satisfaction, {Company Name} has continually raised the bar for excellence in the industry. The latest addition to their extensive product line is the Mission 3x4 Centrifugal Pump, a game-changing innovation that promises to revolutionize the way water is pumped and distributed.The Mission 3x4 Centrifugal Pump is designed to meet the growing demand for efficient, reliable, and high-performance water pumps in a wide range of applications. Whether it's agricultural irrigation, industrial water supply, or municipal water distribution, this innovative pump is engineered to deliver superior performance and unmatched durability. With a maximum flow rate of 1000 gallons per minute and a maximum head of 360 feet, the Mission 3x4 Centrifugal Pump is capable of handling even the most demanding water pumping tasks with ease.One of the key features that sets the Mission 3x4 Centrifugal Pump apart from its competitors is its advanced design and construction. The pump housing is made of high-quality cast iron, ensuring exceptional strength and resistance to corrosion. The impeller and other crucial components are precision-engineered to deliver maximum efficiency and performance, while the heavy-duty bearings and seals are designed to withstand the rigors of continuous operation in tough working environments. In addition, the pump is equipped with a powerful motor that provides reliable and consistent power for extended periods of use.Furthermore, the Mission 3x4 Centrifugal Pump is designed with ease of maintenance and serviceability in mind. Its modular design allows for quick and convenient access to critical components, making inspection, repair, and replacement a breeze. This not only minimizes downtime but also reduces the overall cost of ownership, making it an attractive choice for budget-conscious customers. Moreover, the pump is backed by {Company Name}'s renowned customer support and after-sales service, ensuring peace of mind for customers and maximizing the lifespan of the equipment.Another noteworthy aspect of the Mission 3x4 Centrifugal Pump is its energy efficiency and environmental sustainability. By utilizing state-of-the-art design principles and materials, the pump is able to deliver exceptional performance while minimizing energy consumption. This not only results in cost savings for the end user but also reduces the carbon footprint, contributing to a greener and more sustainable future. In an era where environmental responsibility is paramount, the Mission 3x4 Centrifugal Pump stands out as a shining example of responsible and forward-thinking engineering.As a testament to its outstanding quality and performance, the Mission 3x4 Centrifugal Pump has already garnered attention and accolades from industry experts and customers alike. Its robust construction, cutting-edge technology, and exceptional performance have set a new standard for water pumps, firmly establishing it as a leading innovation in the field. With its versatility and reliability, the pump is poised to make a significant impact in a wide range of industries and applications, meeting the diverse needs of customers around the world.In conclusion, the Mission 3x4 Centrifugal Pump represents the pinnacle of water pump technology, embodying {Company Name}'s unwavering commitment to excellence and innovation. With its outstanding performance, durability, and energy efficiency, it is set to redefine the standards for water pumping equipment, empowering customers with a reliable and efficient solution for their water management needs. As {Company Name} continues to push the boundaries of engineering and manufacturing, the Mission 3x4 Centrifugal Pump stands as a shining example of their dedication to delivering top-quality products that make a positive difference in the world.
Mud Cleaner and Desilter Equipments for China Oil and Gas Industry
China Mud Cleaner and Mud DesilterChina has always been known for its innovation and advancement in technology, and this is no different when it comes to the oil and gas industry. With the increasing demand for efficient drilling operations, China has developed state-of-the-art equipment to meet these demands. One of the key players in this industry is a leading company in China, specializing in the production of high-quality Mud Cleaner and Mud Desilter.The Mud Cleaner and Mud Desilter are essential components in the drilling process, as they are used to remove solid particles and impurities from the drilling mud, ensuring smooth and efficient drilling operations. These machines play a crucial role in maintaining the integrity of the drilling fluid by separating out the solids and allowing the clean mud to be reused.The Mud Cleaner is a combination of a desander, desilter, and a shale shaker, providing a more efficient and compact solution for removing solids from the drilling mud. It is designed to effectively separate and remove the solid particles from the drilling fluid, allowing for the reuse of the clean mud and reducing waste.On the other hand, the Mud Desilter is designed to remove fine solids from the drilling mud, ensuring that the drilling fluid remains in optimal condition for the drilling process. By using hydrocyclones, the Mud Desilter is able to efficiently separate the fine solids from the drilling mud, ensuring that the drilling operation runs smoothly and effectively.The company behind these innovative products is a leading manufacturer and supplier of drilling equipment, with a strong focus on research and development. With cutting-edge technology and a commitment to quality, the company is dedicated to providing solutions that meet the evolving needs of the oil and gas industry.The company's Mud Cleaner and Mud Desilter are designed with the latest advancements in technology, ensuring high performance, efficiency, and reliability. These machines are also designed to withstand the harsh conditions of drilling operations, making them a durable and long-lasting solution for the industry.In addition to their innovative products, the company also provides exceptional customer service and technical support, ensuring that their clients receive the necessary assistance and guidance for their drilling operations. With a team of experienced professionals, the company is able to offer customized solutions to meet the specific requirements of their clients, further reinforcing their commitment to excellence.The company's Mud Cleaner and Mud Desilter have been widely recognized and well-received in the oil and gas industry, with a strong track record of successful installations and operations. Their dedication to quality, innovation, and customer satisfaction has earned them a solid reputation in the industry, making them a trusted and reliable partner for drilling equipment.As the demand for efficient drilling operations continues to grow, the company remains at the forefront of technological advancements, continuously improving and expanding their product line to meet the evolving needs of the industry. With a focus on quality, reliability, and performance, the company continues to set the standard for drilling equipment in the oil and gas industry.In conclusion, China's Mud Cleaner and Mud Desilter, developed by a leading company in the industry, provide a cutting-edge solution for the removal of solid particles and impurities from drilling mud. With a strong focus on quality, innovation, and customer satisfaction, the company has solidified its position as a trusted and reliable partner for drilling equipment in the oil and gas industry. Their commitment to excellence and continuous advancements in technology make them a key player in the industry, ensuring smooth and efficient drilling operations for their clients.
High-Quality Desilter Pump for Effective Waste Management
Desilter Pump: The Ultimate Solution for Efficient Solids ControlIn today's fast-paced and ever-changing industrial landscape, companies are constantly seeking innovative solutions to improve efficiency and reduce operational costs. One crucial aspect of many industrial processes, particularly in the oil and gas, mining, and construction industries, is the effective management of solids and liquids. This is where the revolutionary technology of the Desilter Pump, offered by a leading provider of industrial equipment, comes into play.With a firm commitment to providing cutting-edge solutions for solids control, {Company Name} has established itself as a prominent player in the industry. The company's mission is to empower businesses with the tools and equipment they need to optimize their operations and achieve unparalleled efficiency. In line with this vision, {Company Name} has developed the Desilter Pump, a game-changing solution that is redefining the standards of solids control in industrial settings.At the core of the Desilter Pump's effectiveness is its ability to efficiently remove solid particles from drilling fluids, thereby improving the overall performance of drilling operations. This is achieved through a combination of advanced technologies and precision engineering, resulting in a highly reliable and robust system that delivers consistent results. The Desilter Pump is designed to handle a wide range of operating conditions, making it suitable for a diverse array of industrial applications.One of the key advantages of the Desilter Pump is its ability to enhance the performance of downstream equipment, such as centrifuges and drying shakers, by providing them with clean and fluid-free solids. This not only improves the efficiency of these systems but also extends their operational lifespan, resulting in significant cost savings for businesses. Additionally, the Desilter Pump's compact and portable design makes it easy to deploy and operate in various locations, further adding to its versatility and practicality.The Desilter Pump is also equipped with state-of-the-art control systems that allow for seamless integration with existing equipment and processes. This level of adaptability ensures that businesses can effortlessly incorporate the Desilter Pump into their operations without any disruptions, thereby maximizing its potential impact. Furthermore, the system's user-friendly interface and intuitive controls make it easy for operators to monitor and manage the performance of the Desilter Pump, contributing to a smooth and efficient workflow.In addition to its technical prowess, {Company Name} also places a strong emphasis on customer satisfaction and support. The company's team of experienced professionals is dedicated to providing comprehensive assistance and guidance to clients, ensuring that they are able to leverage the full capabilities of the Desilter Pump. From initial setup and installation to ongoing maintenance and technical support, {Company Name} is committed to being a reliable partner for every customer.The Desilter Pump's success stories are a testament to its impact on businesses across various industries. By investing in this innovative solution, companies have witnessed substantial improvements in their solids control processes, leading to enhanced productivity, reduced downtime, and overall cost savings. With its proven track record and unwavering commitment to excellence, the Desilter Pump has become the go-to choice for businesses seeking a reliable and efficient solids control solution.As industries continue to evolve and demand greater efficiency, the importance of advanced solids control solutions like the Desilter Pump cannot be overstated. {Company Name}'s forward-thinking approach and dedication to innovation have positioned the Desilter Pump as a game-changer in the industry, setting new benchmarks for performance and reliability. With its unparalleled capabilities and unwavering commitment to customer satisfaction, the Desilter Pump is poised to shape the future of solids control in industrial operations.
Top Waste Water Centrifuge Manufacturers for Efficient Water Treatment
**Innovations and Industry Trends in Waste Water Centrifuge Manufacturing**In recent years, the evolving landscape of wastewater treatment has placed significant demands on machinery and technology that can efficiently separate solids from liquids. Among the critical equipment in this sector are waste water centrifuges, devices engineered to accelerate the sedimentation process and enable effective sludge dewatering. Manufacturers in this niche have been driving innovation and adapting to stricter environmental regulations to meet the global push for sustainable water management.Waste water centrifuge manufacturers have been focusing on developing high-performance centrifuges that deliver enhanced separation capabilities, energy efficiency, and durability. These machines are widely used across municipal sewage treatment plants, industrial wastewater processing units, and agricultural runoff management systems. Centrifuge technology, by leveraging high-speed rotation, efficiently segregates suspended solids from wastewater, reducing sludge volume and allowing further treatment or disposal.The company at the center of recent industry discussions has emerged as a leader in this domain, offering cutting-edge centrifuge solutions that align with modern environmental and operational challenges. With decades of experience, their technological expertise is rooted in continuous research and development aimed at optimizing centrifuge designs for diverse waste water profiles.One of the key advances introduced includes enhanced rotor engineering that maximizes centrifugal force without compromising mechanical stability. This advancement allows for higher throughput and improved solid-liquid separation, which is critical for reducing treatment times and operational costs. Additionally, the company has incorporated smart control systems into their centrifuges, enabling real-time monitoring and adaptive operation. These intelligent features allow plant operators to optimize performance dynamically, reduce energy consumption, and anticipate maintenance needs before breakdowns occur.Environmental sustainability is a paramount concern in the wastewater sector, and manufacturers have responded by refining centrifuge technologies to minimize ecological footprint. The company’s centrifuges now feature optimized feed systems and wear-resistant materials that enhance operational lifespan while ensuring consistent output quality. Their designs also prioritize noise reduction and vibration control, addressing environmental and workplace safety standards.Furthermore, the trend toward modular and scalable centrifuge systems is gaining momentum. This approach affords wastewater treatment plants flexibility to expand capacity as demand grows, without committing to oversized initial investments. The company's modular units are engineered to integrate seamlessly within existing infrastructure, simplifying upgrades and reducing downtime.Globally, stricter governmental regulations on wastewater discharge and sludge management intensify the need for efficient solid-liquid separation technologies. The company’s ability to customize centrifuge solutions based on the physicochemical characteristics of different wastewater streams has proven vital in meeting these regulations while maintaining cost-effectiveness. Their teams collaborate closely with clients to tailor system parameters that address local conditions and treatment goals.Industry analysts note that the shift towards digitalization and Industry 4.0 integration in wastewater treatment is opening new frontiers for centrifuge manufacturers. The company has embraced these trends by embedding IoT sensors and cloud connectivity in their equipment. This enables data-driven analytics that support predictive maintenance, operational optimization, and compliance reporting—turning centrifuges from passive pieces of machinery into active components of smart water treatment ecosystems.In addition to technological progress, the company has prioritized aftermarket support and global service networks. By providing comprehensive installation, training, and maintenance programs, they ensure customers derive maximum value from their investments. Their commitment to sustainability extends beyond product design into the full lifecycle, promoting repairability, parts availability, and environmentally responsible disposal practices.As wastewater treatment becomes central to urban planning and industrial sustainability, the role of advanced centrifuge technology cannot be overstated. Emerging challenges such as microplastic removal, changing sludge composition, and energy-conscious operations require ongoing innovation. Waste water centrifuge manufacturers, spearheaded by this company’s forward-thinking developments, are well-positioned to contribute solutions that enhance water reuse, preserve ecosystems, and support circular economy principles.Looking ahead, the company plans to expand its R&D efforts to develop next-generation centrifuge technologies incorporating novel materials, improved automation, and integration with complementary treatment systems such as membrane filtration and bioreactors. By fostering partnerships with research institutions and environmental agencies, they aim to stay at the forefront of water treatment innovation.In conclusion, the wastewater treatment sector is experiencing transformative shifts driven by environmental imperatives and technological advancements. Waste water centrifuge manufacturers are evolving to meet these demands through sophisticated, efficient, and sustainable centrifuge solutions. The company highlighted here exemplifies this progression, delivering tailored equipment that helps clients tackle contemporary wastewater challenges effectively while advancing the global mission of water conservation and pollution reduction. As industries and municipalities continue to prioritize clean water management, the deployment of innovative centrifuge technology will remain crucial to achieving these goals.
Full-Auto Degassing System and Vacuum Degasser for Effective Odor Removal
**China Advances in Environmental Technology with Full-Auto Degassing System and Vacuum Degasser for Odor Removal**In a significant stride towards environmental sustainability and industrial efficiency, China has introduced state-of-the-art full-automatic degassing systems and vacuum degassers designed specifically for effective odor removal. These innovative technologies represent a breakthrough in pollution control and industrial gas treatment, aligning with the nation’s ongoing commitment to ecological protection and green development.### Innovative Degassing Solutions Enhance Environmental ProtectionDegassing systems are critical in various industries for removing unwanted gases and volatile compounds from liquids and industrial emissions. Traditional degassing methods often involve manual operation and limited efficiency, resulting in suboptimal removal of odors and contaminants. The newly developed full-auto degassing systems in China address these challenges by delivering automated, high-precision gas removal processes, significantly improving operational reliability and environmental outcomes.The core of this advancement lies in the automation and vacuum technology integration. Full-automatic degassing systems utilize advanced sensors and control modules to monitor and adjust the degassing operation in real-time. This ensures that the degasser adapts dynamically to varying industrial conditions, maintaining optimal performance while reducing energy consumption and operational costs.Vacuum degassers further enhance the process by operating under reduced pressure conditions, which facilitates the efficient stripping of odor-causing compounds from liquids and gases. This method is particularly effective in industries such as wastewater treatment, chemical manufacturing, and food processing, where the management of malodorous gases is critical to both regulatory compliance and worker safety.### Versatile Applications Across IndustriesChina’s degassing technologies are tailored for multiple industrial applications, demonstrating flexibility and robust performance. In wastewater treatment plants, the systems efficiently remove hydrogen sulfide and other noxious gases, contributing to odor-free operations and improved air quality for surrounding communities. Chemical plants benefit from the precise removal of volatile organic compounds (VOCs), which are major contributors to environmental pollution and health hazards.Furthermore, the food and beverage industry employs these degassing units to eliminate unpleasant odors during production, ensuring product quality and consumer satisfaction. By integrating vacuum degassers into their processing lines, manufacturers can meet stringent hygiene and environmental standards while boosting production efficiency.### Commitment to Green Innovation and SustainabilityThe development and deployment of full-auto degassing systems reflect China’s broader strategy to foster green innovation and tighten environmental regulations. As the country intensifies efforts to reduce industrial emissions and improve air quality, technologies that efficiently address gaseous pollutants and odors are becoming indispensable. These degassing solutions not only help enterprises comply with regulatory frameworks but also demonstrate corporate social responsibility through tangible environmental benefits.### Company Introduction: Pioneers in Degassing TechnologyBehind this technological progress is a leading Chinese company dedicated to advancing gas treatment solutions. With decades of expertise in designing and manufacturing environmental protection equipment, the company combines cutting-edge research with practical industry knowledge to deliver reliable and innovative products.The company’s engineering team focuses on continuous innovation, investing in research and development to enhance system automation, energy efficiency, and operational durability. Their full-auto degassing systems integrate smart control technologies that optimize performance while minimizing human intervention.Moreover, the company provides comprehensive technical support and customized solutions to meet diverse industrial needs. Their vacuum degassers are designed with modular components, allowing easy integration into existing processes and scalable application across various production capacities. This customer-centric approach has earned them a strong reputation in domestic and international markets.### Future Outlook and Industry ImpactLooking ahead, the integration of full-auto degassing systems and vacuum degassers is expected to become a standard in China’s industrial pollution control landscape. As environmental standards continue to tighten, companies across sectors will increasingly adopt such advanced technologies to ensure compliance and enhance process efficiencies.Additionally, the success of these systems promotes further research into automation and vacuum technologies, potentially leading to new applications and improved environmental solutions. The synergy between technological innovation and sustainability goals highlights China’s leadership role in global environmental management.### ConclusionChina’s introduction of full-automatic degassing systems and vacuum degassers for odor removal represents a notable achievement in industrial environmental technology. By combining automation with vacuum technology, these systems offer effective, energy-efficient solutions for controlling industrial odors and gaseous pollutants. Supported by a leading manufacturer with deep industry expertise, these innovations pave the way for enhanced environmental protection, regulatory compliance, and sustainable industrial growth. As China continues to prioritize ecological preservation and technological advancement, such developments will play a crucial role in achieving a cleaner, healthier future.
Effective Drilling Mud Solid Control System and Rig Solid Control System for Drilling Operations in China
China Drilling Mud Solid Control System and Solid Control System for Drilling RigChina is a leading force in the innovation and production of drilling mud solid control systems and solid control systems for drilling rigs. These systems play a crucial role in the oil and gas industry, as they are responsible for the efficient and effective removal of drilling cuttings and other solid particles from the drilling mud, thus ensuring the smooth operation of drilling rigs and the protection of drilling equipment.One company that has been at the forefront of developing and manufacturing these essential systems is {}. With years of experience and a commitment to excellence, they have established themselves as a trusted and reliable provider of drilling mud solid control systems and solid control systems for drilling rigs.The drilling mud solid control system is an integral part of the drilling process, as it helps to maintain the proper properties of the drilling mud, including its density, viscosity, and pH level. This is crucial for ensuring the stability of the borehole, preventing blowouts, and protecting the drilling equipment. The system typically consists of several components, including shale shakers, desanders, desilters, decanter centrifuges, and mud cleaners, all of which work together to remove solid particles from the drilling mud.Similarly, the solid control system for drilling rigs is responsible for the efficient removal of the drilling cuttings from the drilling mud, thus ensuring the smooth and uninterrupted operation of the drilling rig. This system typically includes equipment such as shale shakers, mud cleaners, centrifuges, and degassers, all of which help to separate the solid particles from the drilling mud and prevent them from building up in the drilling rig.{} has developed a comprehensive range of drilling mud solid control systems and solid control systems for drilling rigs to meet the diverse needs of their customers. Their systems are designed to deliver high performance, reliability, and ease of maintenance, thus helping drilling operators to maximize efficiency and reduce downtime. With a strong focus on research and development, they are constantly striving to improve their systems and develop innovative solutions to meet the evolving needs of the oil and gas industry.In addition to manufacturing high-quality systems, {} also provides comprehensive technical support and after-sales services to their customers. This includes installation, commissioning, training, maintenance, and troubleshooting, thus ensuring that their customers can operate their drilling mud solid control systems and solid control systems for drilling rigs with confidence and peace of mind.Moreover, {} places a strong emphasis on environmental protection and sustainability in the design and production of their systems. They are committed to developing systems that minimize environmental impact by reducing waste, energy consumption, and emissions, thus helping their customers to operate in a more environmentally responsible manner.As a leading provider of drilling mud solid control systems and solid control systems for drilling rigs, {} has established a strong presence in both domestic and international markets. Their systems have been widely adopted by drilling operators and contractors in various regions around the world, and they have earned a reputation for delivering exceptional performance, reliability, and value.Looking ahead, {} is poised to continue its leadership in the development and production of drilling mud solid control systems and solid control systems for drilling rigs. With a focus on innovation, quality, and customer satisfaction, they are well-positioned to meet the ever-growing demand for these essential systems and to contribute to the advancement of the oil and gas industry.In conclusion, China is a key player in the development and production of drilling mud solid control systems and solid control systems for drilling rigs, and companies like {} are leading the way in delivering high-performance, reliable, and environmentally responsible systems to the market. As the demand for these systems continues to grow, it is clear that China will play a crucial role in shaping the future of the oil and gas industry.
Solid Liquid Separator and 3-Phase Separation Filter for Industrial Use in China
China Solid Liquid Separator and 3-Phase Separation FilterIn the world of industrial manufacturing, the need for efficient and reliable solid-liquid separation solutions is paramount. This is where the China Solid Liquid Separator and 3-Phase Separation Filter, developed by [company name], comes into play. This innovative product offers a range of benefits to industries such as wastewater treatment, food processing, mining, and oil and gas production, making it a vital tool for businesses worldwide.The China Solid Liquid Separator and 3-Phase Separation Filter is designed to effectively separate solid and liquid components from a mixture, providing a high level of efficiency and precision. By utilizing advanced filtration technology, this product is able to remove contaminants and impurities from a variety of substances, resulting in a cleaner and more refined end product.One of the key features of the China Solid Liquid Separator and 3-Phase Separation Filter is its versatility. This product is capable of handling a wide range of materials, including sludge, slurries, and other complex mixtures. This flexibility makes it an ideal solution for industries with diverse separation needs, allowing for seamless integration into existing production processes.In addition to its solid-liquid separation capabilities, the China Solid Liquid Separator and 3-Phase Separation Filter also offers a unique 3-phase separation function. This feature allows for the simultaneous extraction of oil, water, and solid particles from a mixture, further enhancing its utility in industries such as oil and gas production.[company name] is at the forefront of the development and manufacturing of innovative separation solutions. With a strong focus on research and development, the company has consistently delivered cutting-edge products that address the evolving needs of modern industries.The China Solid Liquid Separator and 3-Phase Separation Filter is a testament to [company name]'s commitment to excellence and innovation. By leveraging the latest technological advancements, the company has created a product that sets a new standard for solid-liquid separation, offering unmatched performance and reliability.As a leading provider of separation solutions, [company name] is dedicated to supporting its customers with top-quality products and exceptional service. The China Solid Liquid Separator and 3-Phase Separation Filter is backed by the company's extensive technical expertise, ensuring that customers receive the support they need to maximize the benefits of this innovative product.In conclusion, the China Solid Liquid Separator and 3-Phase Separation Filter represents a significant advancement in solid-liquid separation technology. With its exceptional performance, versatility, and 3-phase separation capabilities, this product is poised to make a lasting impact on a wide range of industries. Backed by [company name]'s unwavering commitment to excellence, the China Solid Liquid Separator and 3-Phase Separation Filter is set to become a cornerstone of modern industrial manufacturing.
Discover the Versatility of Flat Shaker Screens for Effective Solid Separation
FLC 500 Flat Shaker Screen: Revolutionizing the Drilling IndustryThe drilling industry is constantly evolving, with new technologies and equipment constantly emerging to improve efficiency and operational capabilities. One such innovation making waves in the sector is the FLC 500 Flat Shaker Screen, a groundbreaking solution developed by a prominent industry player.Designed to enhance the performance and productivity of drilling operations, the FLC 500 Flat Shaker Screen is revolutionizing the way drilling companies approach their work. With its advanced features and engineering excellence, this game-changing technology has gained significant recognition within the industry.The FLC 500 Flat Shaker Screen is the result of extensive research and development by a leading drilling equipment manufacturer. Leveraging their rich experience and expertise, the company identified a need for an improved shaker screen solution to overcome the challenges faced by drilling companies.One of the key features that sets the FLC 500 Flat Shaker Screen apart from its competitors is its flat design. This innovative construction ensures optimal solids control, allowing for more efficient separation of drilling fluids and solids during the drilling process. The flat screen surface provides a larger area for fluid dewatering, maximizing the screen's capacity and performance.Additionally, the FLC 500 Flat Shaker Screen boasts enhanced durability and longevity. Crafted using high-quality materials and state-of-the-art manufacturing techniques, this robust solution withstands the harsh operating conditions typically encountered in drilling operations. Its extended lifespan not only reduces operational downtime but also significantly lowers maintenance and replacement costs.Furthermore, the FLC 500 Flat Shaker Screen offers exceptional versatility. Compatible with various drilling equipment, it seamlessly integrates with existing systems, ensuring a hassle-free installation process. Its adaptability empowers drilling companies to upgrade their equipment without requiring substantial modifications, thereby improving operational efficiency and saving valuable time.The company behind this breakthrough innovation is known for its commitment to delivering superior technology with a focus on customer satisfaction. With a relentless dedication to research and development, combined with a customer-centric approach, they have earned a reputation as a trusted and reliable partner in the drilling industry.The FLC 500 Flat Shaker Screen is just one example of the company's commitment to innovation. Their extensive product portfolio includes a range of drilling equipment tailored to meet the unique needs and challenges of the industry. From screens to pumps, they offer comprehensive solutions that cater to diverse drilling requirements.In addition to their cutting-edge technology, the company places great emphasis on customer support and service. Their team of highly skilled professionals provides industry-leading technical assistance and on-site support to ensure seamless integration and optimal performance of their equipment. This dedication to customer satisfaction has positioned them as a preferred supplier amongst drilling companies worldwide.The introduction of the FLC 500 Flat Shaker Screen marks a significant milestone in the drilling industry. With its flat design, enhanced durability, and unmatched versatility, it is transforming the way drilling operations are conducted. As companies continue to prioritize efficiency and productivity, this revolutionary technology is set to play a pivotal role in shaping the future of the drilling industry.
Top Waste Water Centrifuge Manufacturers for Efficient Wastewater Treatment
**Innovations in Waste Water Treatment: The Rise of Advanced Centrifuge Technologies**In the realm of environmental management and industrial wastewater treatment, the demand for efficient, reliable, and cost-effective solutions has never been higher. As industries expand and urban populations grow, managing wastewater effectively is crucial for sustainable development and environmental protection. Among the various technologies leveraged in this sector, waste water centrifuges have emerged as a pivotal component, enabling enhanced sludge dewatering and solid-liquid separation processes.Waste water centrifuges are mechanical devices that utilize centrifugal force to separate solids from liquids in wastewater streams. This separation is essential for reducing the volume of sludge, thereby lowering disposal costs and environmental impact. The continuous evolution of centrifuge technology has led to more advanced designs that offer higher throughput, improved separation efficiency, and greater energy savings.**Market Landscape and Technological Advancements**Recent developments in waste water centrifuge manufacturing reflect a broader industry trend towards automation, durability, and environmental compliance. Modern centrifuges incorporate sophisticated control systems that optimize operating parameters in real time, ensuring consistent performance even under varying feed conditions. Material innovations, such as corrosion-resistant alloys and reinforced composites, extend equipment lifespan and reduce maintenance requirements.Manufacturers are also focusing on compact and modular designs that allow for easier installation and integration into existing treatment plants. These improvements are especially beneficial for municipal wastewater treatment facilities and industrial operations facing space constraints or seeking to upgrade aging infrastructure without extensive civil works.Moreover, energy efficiency remains a key focus area. New centrifuge models consume significantly less power, aligning with global efforts to reduce carbon footprints and operational costs. Enhanced solids capture rates also facilitate the production of drier sludge cakes, which streamline transportation and biomass conversion processes.**Company Introduction**[The company] has established itself at the forefront of waste water centrifuge innovation, providing tailored solutions that meet the unique challenges of diverse industries such as chemical manufacturing, food processing, pharmaceuticals, and municipal wastewater treatment. With decades of expertise, the company designs and manufactures centrifuges that strike a balance between robust mechanical performance and user-friendly operation.By investing heavily in research and development, the company continuously integrates cutting-edge technologies, including smart sensors and automation software, into its product lineup. This commitment ensures that clients benefit from maximum process efficiency, minimal downtime, and simplified maintenance procedures.Additionally, the company offers comprehensive after-sales support, including installation services, operator training, and prompt technical assistance. Through this customer-centric approach, it builds long-term partnerships aimed at optimizing wastewater treatment processes and achieving sustainability goals.**Applications and Industry Impact**Waste water centrifuges produced by leading manufacturers serve critical roles across a spectrum of applications. In municipal treatment plants, centrifuges help manage large volumes of sludge generated during primary and secondary treatment stages. By efficiently separating solids, the overall treatment cycle becomes more manageable, and the risk of environmental contamination decreases substantially.In industrial sectors, wastewater often contains complex contaminants and high levels of suspended solids requiring robust separation technologies. For example, in pharmaceutical and chemical plants, centrifuges must withstand corrosive and abrasive materials while delivering reliable performance. Advanced centrifuges from top manufacturers provide the resilience and efficiency needed to meet these stringent requirements.Food and beverage industries benefit from customized centrifuge systems designed to handle variable sludge compositions and flow rates. These systems contribute to improved water reuse and compliance with environmental regulations, thereby supporting sustainable production practices.**Sustainability and Future Trends**As environmental regulations become more stringent and sustainability takes center stage, waste water centrifuge manufacturers are shaping the future of wastewater management. Innovations such as integration with IoT platforms enable real-time performance monitoring and predictive maintenance, reducing unplanned outages and extending equipment life.Emerging trends also include the development of hybrid separation technologies that combine centrifugation with membrane filtration or other advanced methods, further enhancing treatment efficacy. Additionally, there is a growing emphasis on designing centrifuges that accommodate alternative sludge treatment methods, including anaerobic digestion and resource recovery pathways.The shift towards circular economy principles incentivizes manufacturers and end-users alike to optimize sludge management for beneficial reuse, turning waste into valuable secondary resources such as biogas, biofertilizers, and raw materials for construction.**Conclusion**The advancements in waste water centrifuge technology reflect an industry committed to meeting the escalating demands of environmental stewardship and industrial efficiency. Companies specializing in this field offer comprehensive solutions that not only improve sludge dewatering and separation but also contribute significantly to sustainability efforts.Through superior design, technological integration, and dedicated support services, waste water centrifuge manufacturers play a vital role in enabling industries and municipalities to manage their wastewater challenges effectively. As this sector continues to evolve, it promises even greater contributions towards cleaner water resources and a healthier planet.