Decanter Centrifuge Diagram Explained: How It Works and Key Components
By:Admin
Company News & Blog
Effective Mud Gas Separator for Oil and Gas Drilling Operations
[Company Name] Introduces New Mud Gas Separator for Safer Drilling Operations[City, State] - [Company Name], a global leader in drilling equipment and technology, has introduced a new Mud Gas Separator to their extensive line of products. The Mud Gas Separator is designed to improve safety and efficiency in drilling operations, providing a reliable solution for removing harmful gases from the drilling fluid.The Mud Gas Separator is a vital component in the drilling process, as it helps to prevent the buildup of dangerous gases such as methane, carbon dioxide, and hydrogen sulfide. These gases can pose serious risks to both personnel and equipment on the drilling rig, making the efficient removal of these gases a top priority. With the introduction of their new Mud Gas Separator, [Company Name] aims to provide their customers with a state-of-the-art solution to effectively manage gas while drilling.The [Company Name] Mud Gas Separator features a high-efficiency design that effectively separates and vents gas from the drilling fluid, ensuring a safe and controlled environment on the rig. This advanced technology reduces the risk of gas-related incidents and improves overall drilling performance. Additionally, the Mud Gas Separator is built to withstand the harsh conditions of drilling operations, offering durability and reliability in the field.[Company Name] has a long-standing reputation for delivering innovative and high-quality equipment to the oil and gas industry. With a focus on safety, efficiency, and environmental stewardship, the company continues to develop cutting-edge solutions to meet the evolving needs of their customers. The introduction of the Mud Gas Separator is a testament to their commitment to providing industry-leading equipment that enhances operational performance and minimizes risk."We are thrilled to introduce our new Mud Gas Separator to the market," said [Spokesperson], [Title] at [Company Name]. "Safety is a top priority for us, and we believe that this new product will significantly improve the safety and efficiency of drilling operations. The Mud Gas Separator is a testament to our dedication to providing reliable solutions that address the challenges our customers face in the field."In addition to the Mud Gas Separator, [Company Name] offers a comprehensive range of drilling equipment and services, including drilling rigs, drilling tools, well control systems, and more. Their global presence and extensive industry expertise make them a trusted partner for drilling contractors and operators around the world.As the oil and gas industry continues to push the boundaries of exploration and production, the demand for advanced equipment that enhances safety and performance remains strong. With the introduction of the Mud Gas Separator, [Company Name] is well-positioned to meet this demand and support the industry in achieving its goals.For more information about the [Company Name] Mud Gas Separator and their complete range of drilling solutions, visit [website].
Comparison of Derrick FLC 513 and Swaco Mongoose Equipment Equivalents
Certainly! Please provide the company introduction you’d like me to include, and I will craft an 800-word news article that discusses the China Derrick FLC 513 Equivalence and Swaco Mongoose Equivalence without mentioning brand names.
High Quality Sugar Syrup Pump and Transfer Pump from China
China Sugar Syrup Pump and Sugar Syrup Transfer Pump, are widely used in the food and beverage industry for transferring sugar syrups, honey, molasses, and other viscous liquids. These pumps are designed to handle the challenges of transferring high viscosity and sticky fluids in a hygienic and efficient manner.The sugar syrup pump is designed to handle the thick and sticky nature of sugar syrup, which can be a challenging task for standard pumps. The pump is equipped with a special design that allows it to handle the high viscosity of sugar syrup without clogging or losing efficiency. This ensures the smooth and continuous transfer of sugar syrup, eliminating any downtime or production delays.Similarly, the sugar syrup transfer pump is designed for transferring large quantities of sugar syrup from one location to another within a food or beverage production facility. The pump is capable of handling the high flow rates required for transferring large volumes of sugar syrup, making it an essential component in the production process.Both pumps are manufactured using high-quality materials, such as stainless steel or food-grade plastics, to ensure the highest level of hygiene and safety for food and beverage production. This makes them suitable for use in the most demanding sanitary environments, including in the production of confectionery, beverages, and baked goods.The company behind these innovative pumps, [Company Name], is a leading manufacturer and supplier of fluid handling equipment for the food and beverage industry. With years of experience and expertise in the field of fluid handling, the company has gained a reputation for providing high-quality and reliable solutions for the transfer of viscous and sticky fluids.[Company Name] is committed to delivering innovative and efficient solutions to its customers, and the sugar syrup pump and sugar syrup transfer pump are a testament to this commitment. The company's team of engineers and technical experts have worked tirelessly to develop pumps that are specifically tailored to the unique challenges of transferring sugar syrups and other viscous liquids in the food and beverage industry.In addition to their superior performance, the sugar syrup pump and sugar syrup transfer pump are also designed with ease of maintenance and cleaning in mind. This ensures that the pumps can be easily disassembled, cleaned, and reassembled without any hassle, contributing to the overall efficiency and productivity of the production process.The company also offers comprehensive technical support and after-sales service for its pumps, ensuring that customers can rely on the continued performance and reliability of their equipment. This commitment to customer satisfaction sets [Company Name] apart as a trusted partner for fluid handling solutions in the food and beverage industry.With the increasing demand for high-quality and efficient fluid handling equipment in the food and beverage industry, the sugar syrup pump and sugar syrup transfer pump from [Company Name] are well-positioned to meet the evolving needs of food and beverage producers. Their ability to handle the unique challenges of transferring sugar syrups and other viscous liquids makes them an indispensable asset for any production facility.In conclusion, the sugar syrup pump and sugar syrup transfer pump from [Company Name] are a testament to the company's dedication to providing innovative and efficient solutions for the food and beverage industry. With their superior performance, hygienic design, and ease of maintenance, these pumps are set to make a significant impact on the production of confectionery, beverages, and baked goods. As the industry continues to evolve, [Company Name] remains at the forefront of providing reliable and high-quality fluid handling equipment for its customers.
Top 5 Essential Solid Control Equipment for Oil and Gas Industry
Solid Control Equipment, a leading provider of innovative equipment and services for the oil and gas industry, has recently made significant advances in their technology to improve drilling operations. With a commitment to providing cutting-edge solutions for their clients, Solid Control Equipment has solidified its position as a trusted partner in the industry.Founded in [year], Solid Control Equipment has built a strong reputation for delivering high-quality equipment and services to the oil and gas sector. The company's dedicated team of engineers and technicians work tirelessly to develop and manufacture state-of-the-art equipment that meets the evolving needs of the industry. Their unwavering commitment to innovation and excellence has propelled Solid Control Equipment to the forefront of the market.One of the company's most recent developments is the introduction of advanced solid control equipment that is designed to optimize drilling operations. This new equipment incorporates the latest technologies to enhance drilling efficiency and minimize environmental impact. By effectively managing the drilling fluid, Solid Control Equipment's innovative solutions help to ensure smooth operations and reduce the need for costly downtime.In addition to their cutting-edge equipment, Solid Control Equipment also offers a comprehensive range of services to support their clients' operations. From installation and maintenance to technical support and training, the company's team of experts is dedicated to providing a seamless experience for their customers. Their commitment to exceptional service has earned them a loyal customer base and a strong reputation for reliability and expertise.Solid Control Equipment's success can be attributed to their relentless pursuit of excellence and their focus on meeting the unique needs of each client. By understanding the challenges and requirements of the oil and gas industry, the company is able to develop tailored solutions that deliver tangible results for their customers. Their ability to adapt to changing market dynamics and embrace new technologies has positioned them as a leader in the industry.The company's commitment to sustainability is also evident in their approach to product development and operations. Solid Control Equipment places a strong emphasis on environmental responsibility, ensuring that their equipment and services are designed with the utmost consideration for minimizing their ecological footprint. By prioritizing sustainable practices, the company is able to support their clients in meeting their own environmental objectives.As the oil and gas industry continues to evolve, Solid Control Equipment remains at the forefront, driving innovation and delivering value to their clients. With a track record of success and a steadfast dedication to excellence, the company is poised for continued growth and success in the years to come. By leveraging their expertise and forward-thinking approach, Solid Control Equipment is well-positioned to meet the evolving needs of the industry and maintain their position as a trusted leader in the market.
Hotplate Stirrer and Lab Magnetic Stirrer for Precise Laboratory Mixing
**Innovative Advances in Laboratory Equipment: China Hotplate Stirrer and Lab Magnetic Stirrer Make Waves in Scientific Research**In the rapidly evolving landscape of scientific research and development, laboratory equipment plays a pivotal role in driving innovation and ensuring precise experimental outcomes. Among these essential tools, the hotplate stirrer and magnetic stirrer stand out for their versatility and efficiency. Recent developments in China's manufacturing of these devices have garnered significant attention from researchers and industry experts worldwide.### Rising Demand for Quality Laboratory EquipmentThe increasing complexity of scientific experiments, spanning fields such as chemistry, biology, pharmaceuticals, and materials science, necessitates equipment that combines reliability, accuracy, and ease of use. Two laboratory instruments—the hotplate stirrer and the magnetic stirrer—are fundamental in many experimental protocols. They facilitate uniform heating and mixing of liquids, which are critical for reactions, solution preparations, and sample analysis.China, as one of the leading manufacturers of laboratory equipment, has made substantial progress in enhancing the design, performance, and affordability of these devices. The surge in research activities, coupled with the need for cost-effective instruments, has positioned Chinese hotplate stirrers and lab magnetic stirrers as attractive options for laboratories globally.### Features and Benefits of the Hotplate StirrerThe hotplate stirrer is a multifunctional device combining heating and stirring capabilities on a single platform. This dual functionality allows scientists to conduct experiments requiring simultaneous temperature control and agitation, such as dissolving solids into liquids, accelerating chemical reactions, or maintaining homogenous mixtures.Modern hotplate stirrers made in China incorporate advanced temperature sensors and electronic controls, enabling precise temperature regulation usually up to several hundred degrees Celsius with minimal fluctuation. Safety features such as over-temperature protection and non-slip surfaces enhance user confidence and reduce the risk of accidents.Moreover, these hotplate stirrers often come with variable speed control for the stirring function, allowing researchers to customize the mixing speed based on the viscosity and nature of the solution. The magnetic stirring mechanism employs strong magnets beneath the plate, which magnetically couple with a stir bar placed inside the liquid container, ensuring consistent and contamination-free stirring.### Advantages of Lab Magnetic StirrersLab magnetic stirrers, while lacking a heating element, are indispensable when only homogenization or agitation is required without temperature elevation. Their compact size and simplicity make them ideal for delicate procedures where heat-sensitive substances are involved or where temperature control is managed separately.Chinese-manufactured magnetic stirrers feature robust magnetic coupling, adjustable stir speeds, and durable construction materials that resist corrosion and ensure longevity. Many models are designed for energy efficiency and quiet operation, an important factor for maintaining a distraction-free laboratory environment.Furthermore, technological advancements have introduced digital displays and programmable settings to magnetic stirrers, allowing researchers to replicate stirring conditions precisely across multiple experiments, thereby enhancing reproducibility and reliability of results.### Meeting International Standards and CustomizationAnother key aspect driving the popularity of Chinese hotplate and magnetic stirrers is compliance with stringent international quality standards such as ISO, CE, and RoHS certifications. Manufacturers employ rigorous quality control processes to ensure each device meets global safety and performance benchmarks.In addition, manufacturers often offer customization options tailored to specific research needs. Options include varying plate sizes, digital versus analog interfaces, compatibility with different vessel types, and integration with laboratory automation systems. This flexibility enables laboratories to select equipment that perfectly aligns with their workflow requirements and budget constraints.### Company ProfileEstablished as a forefront player in the scientific equipment sector, the company behind these innovative laboratory instruments has a rich history of commitment to research excellence and customer satisfaction. With a dedicated R&D team, state-of-the-art manufacturing facilities, and a global distribution network, the company continues to push the boundaries of laboratory technology.Customer-centric approaches, including after-sales support, training programs, and technical consultancy, have cemented the company’s reputation as a trusted partner among academic institutions, pharmaceutical enterprises, and industrial laboratories alike.### Impact on Scientific Research and IndustryThe availability of efficient, cost-effective hotplate stirrers and magnetic stirrers from China is catalyzing advancements in experimental research worldwide. Enhanced accessibility to quality equipment empowers scientists to undertake complex experiments with greater confidence and consistency.Pharmaceutical research benefits particularly from these instruments, where precise temperature control and mixing are crucial in drug formulation and development. Similarly, in chemical synthesis and materials science, the reliability of these devices aids in scaling up reactions from laboratory benches to pilot and production scales.Beyond research, educational institutions also gain from these advancements. Affordable and user-friendly laboratory stirrers enable hands-on learning experiences for students, nurturing the next generation of scientists and engineers.### Looking AheadAs scientific demands continue to grow, the evolution of hotplate and magnetic stirrers will likely incorporate smart technologies such as IoT connectivity, remote monitoring, and AI-driven process optimization. Chinese manufacturers are well-positioned to lead these innovations, supported by robust industrial infrastructure and a proactive approach to technological trends.In conclusion, the ongoing improvements in China's hotplate stirrer and lab magnetic stirrer offerings underline the country’s increasing influence in the global laboratory equipment market. Combining quality, innovation, and affordability, these devices are instrumental in advancing scientific discovery and industrial progress across the globe.
Efficient Mud Vacuum Degasser: A Vital Solution for Effective Mud Separation
In today's world, the oil and gas industry has been one of the most critical sectors, driving the economic growth of many countries. The industry has proven to be an excellent source for the production and provision of many resources necessary for human existence. The success of the industry has been attributed to the use of advanced technology and innovation.Mud vacuums degasser is one such technology that has been used to improve the efficiency of drilling operations in the oil and gas sector. Through this technology, drilling operations have become more environmentally friendly and cost-effective. Mud vacuum degassers help in the removal of harmful hydrocarbon gases and mud from drilling fluids.Leading companies in the oil and gas industry, such as (need remove brand name), have invested heavily in the research and development of mud vacuum degassers. The company realizes the importance of such technology to their clients, and as such, they have produced some of the best mud vacuum degassers in the market.Mud vacuum degassers have several advantages that have made them a favorite among drilling companies. Below are some of the benefits of mud vacuum degassers:1. EfficiencyThe main aim of mud vacuum degasser is to remove harmful hydrocarbon gases and mud from drilling fluids used in drilling operations. This process has been proven to be effective in minimizing the occurrence of accidents during drilling. It increases the efficiency of drilling operations and minimizes downtime by removing the contaminants in drilling fluids.2. Environmental BenefitsThe use of mud vacuum degassers has significantly reduced the impact of oil and gas exploration on the environment. Drilling fluids that contain harmful hydrocarbon gases and mud can cause environmental pollution and damage to surrounding ecosystems. The use of mud vacuum degassers ensures that such pollutants are removed before they can cause any harm.3. Cost-EffectiveMud vacuum degassers have been proven to be cost-effective, buying a good mud vacuum degasser (need remove brand name) can save drilling companies thousands of dollars in costs related to accidents, downtime, and environmental damage. The technology reduces maintenance costs, as well as repair and replacement costs, that could arise from the use of conventional drilling techniques.The mud vacuum degassers manufactured by (need remove brand name) are of high quality and are designed to meet the unique needs of different drilling companies. The company has a team of highly skilled engineers who continually research and improve mud vacuum degassing technology.One of the primary advantages of (need remove brand name) mud vacuum degassers is that they are rugged and durable, making them ideal for use in harsh environments. The mud vacuum degassers are equipped with a large diameter exhaust, which allows for efficient handling of larger volumes of drilling fluids.The company also uses state-of-the-art technology in the manufacturing of their mud vacuum degassers, ensuring that the products meet the highest quality standards in the industry. (need remove brand name) mud vacuum degassers are designed to meet various regulatory requirements, including those set by the Occupational Safety and Health Administration (OSHA).In conclusion, the use of mud vacuum degassers in the oil and gas industry has significantly improved the efficiency and safety of drilling operations. The technology has also led to a reduction in environmental damage and a considerable cost reduction for drilling companies. (need remove brand name) is a leading manufacturer of mud vacuum degassers and their products have been proven to be effective and durable. The company's commitment to research and development ensures that they continue to produce state-of-the-art mud vacuum degassers that meet the unique needs of the industry.
Revolutionary Palm Oil Sludge Decanter Centrifuge Optimizes Separation Process in Malaysia
Palm Oil Sludge Separation Made Effortless with Decanter Centrifuges from ChinaPalm oil production is among the largest agricultural industries not only in Malaysia but also across the globe. With increased demand for palm oil, more and more industries are joining the race to tap into this lucrative business. However, the process of producing palm oil usually results in a lot of waste material, with sludge being among the most significant. Sludge is usually composed of residual oil, water, and solid debris, making it an environmental hazard when not properly disposed of. Luckily, with the advancement in technology, companies such as ZK Separation have come up with decanter centrifuges that make sludge separation easier and more efficient.ZK Separation's decanter centrifuges provide the ultimate solution in the palm oil sludge separating process. They are designed to separate the residual oil from the water by utilizing high centrifugal force. The decanter centrifuges have a unique and innovative design that guarantees maximum efficiency and high-quality separation. Not only do the decanters remove the oil, but they also help remove impurities, making it easier to dispose of the sludge.The China crude oil centrifuge and olive oil decanter centrifuge from ZK Separation are some of the most widely used machines in palm oil sludge separation. Their unrivaled performance and high efficiency rates have made them a favorite among clients across the globe. The company has invested heavily in research and development to ensure that their machines are of the highest quality.The China crude oil centrifuge is specially designed to make crude oil separation easier and more efficient. The machine has a robust construction that can handle various crude oil types, including palm oil. Its critical components such as the bowl and conveyor are made using high-quality materials to guarantee maximum durability and longevity.Similarly, the olive oil decanter centrifuge is also designed to make the separation of olive oil from water and other solid materials easier. The machine has undergone extensive testing and refinement to ensure maximum performance. Its automatic control system makes it easy to operate and customize according to the user's needs.In conclusion, the separation of palm oil sludge is an essential process in ensuring environmental sustainability in the palm oil industry. ZK Separation is at the forefront of designing innovative and efficient decanter centrifuges that make the process easier and more efficient. The China crude oil centrifuge and olive oil decanter centrifuge from the company have proven to be reliable and efficient in the separation process, making them a must-have for any industry player.
Drilling Mud Circulation System Overview and Benefits
**Innovative Drilling Mud Circulation System Enhances Efficiency and Safety in Oil and Gas Operations**In the continuously evolving oil and gas industry, the efficiency and reliability of drilling operations significantly impact overall productivity and safety. A recent advancement in drilling technology — the Drilling Mud Circulation System — promises to revolutionize the way drilling mud is managed on-site, offering enhanced performance, environmental benefits, and operational cost reductions.### What is the Drilling Mud Circulation System?The Drilling Mud Circulation System (DMCS) is an integrated solution designed to optimize the handling and circulation of drilling fluids during the drilling process. Drilling mud, a specialized fluid mixture, plays a critical role in lubricating and cooling the drill bit, stabilizing the borehole walls, carrying cuttings to the surface, and balancing subterranean pressures.Traditional systems often face challenges such as inefficiencies in mud recycling, environmental contamination risks, and equipment wear and tear. The DMCS addresses these issues through advanced engineering and automation, ensuring continuous circulation, precise control, and improved mud properties throughout the drilling cycle.### Key Features and Benefits1. **Enhanced Operational Efficiency** The system incorporates state-of-the-art pumps, separators, and filtration units that work seamlessly to maintain optimal mud properties. Real-time monitoring sensors provide data on fluid density, viscosity, and contaminant levels, enabling operators to make informed adjustments promptly. This reduces downtime caused by mud-related complications and expedites drilling progress.2. **Environmental Protection** Environmental regulations in oil and gas extraction are becoming increasingly stringent. The DMCS includes advanced separation technology that significantly lowers the amount of residual solids and pollutants released into the environment. By maximizing mud recycling and minimizing waste, the system helps drilling companies meet compliance requirements and reduce their ecological footprint.3. **Improved Safety Measures** Handling drilling mud involves risks due to chemical composition and machinery. The enclosed system design minimizes human exposure to hazardous substances and reduces the risk of spills and leaks. Automated controls and fail-safe mechanisms further enhance site safety by preventing equipment failures and enabling quick response to anomalies.4. **Cost Reduction and Resource Optimization** Efficient mud circulation means less frequent need for new mud preparation and disposal, which translates to operational cost savings. Additionally, by preventing equipment damage and reducing maintenance intervals, the system extends the life span of critical components.### Application in Diverse Drilling EnvironmentsThe versatile design of the DMCS makes it suitable for various drilling environments, including onshore and offshore platforms, unconventional resource extraction, and deepwater drilling projects. Its modular configuration allows customization based on specific operational requirements, ensuring compatibility with existing rig infrastructure.### About the Company Behind the InnovationThe developer of this cutting-edge Drilling Mud Circulation System is a leading player in the oilfield services sector, with decades of expertise in designing and manufacturing advanced drilling equipment. The company is committed to fostering innovation that addresses the evolving needs of the energy industry while prioritizing safety, environmental stewardship, and customer satisfaction.Founded over 30 years ago, the company has earned a reputation for delivering robust, high-performance products that enhance drilling efficiency. With a global footprint and a team of experienced engineers and technicians, the company continuously invests in research and development to stay ahead of industry trends and challenges.Its portfolio encompasses a wide range of drilling solutions, including drilling rigs, mud pumps, well control equipment, and monitoring systems. By integrating the DMCS into its product lineup, the company reinforces its dedication to providing comprehensive, end-to-end solutions that optimize drilling operations from start to finish.### Industry Impact and Future ProspectsThe introduction of the Drilling Mud Circulation System arrives at a pivotal moment when the oil and gas sector is under pressure to improve operational efficiency and sustainability simultaneously. Early adopters of the system have reported notable improvements in drilling turnaround times and reductions in fluid handling costs.Looking ahead, the company plans to enhance the system’s capabilities by incorporating artificial intelligence and machine learning algorithms to predict and preempt potential mud-related issues. Such technological integration is expected to further revolutionize drilling fluid management, making operations smarter and more adaptive.In addition, collaborations with environmental agencies and industry partners aim to refine the system’s environmental performance and develop best practices for responsible drilling mud management. These efforts align with broader industry initiatives to promote sustainable resource exploration.### ConclusionThe Drilling Mud Circulation System represents a significant advancement in drilling technology, offering a comprehensive solution to longstanding challenges in mud management. By improving efficiency, safety, and environmental compliance, this innovation contributes to the modernization of the oil and gas industry.Backed by a reputable company with a strong track record and commitment to innovation, the DMCS is set to become a standard component in drilling operations worldwide. As the energy sector continues to navigate complex technical and regulatory landscapes, such sophisticated systems will be instrumental in driving progress and sustainable development.---*For more information about the Drilling Mud Circulation System and other drilling technologies, please contact the company’s sales and technical support teams or visit their official website.*
New Mixing Hopper Technology: A Game Changer in Industrial Processing
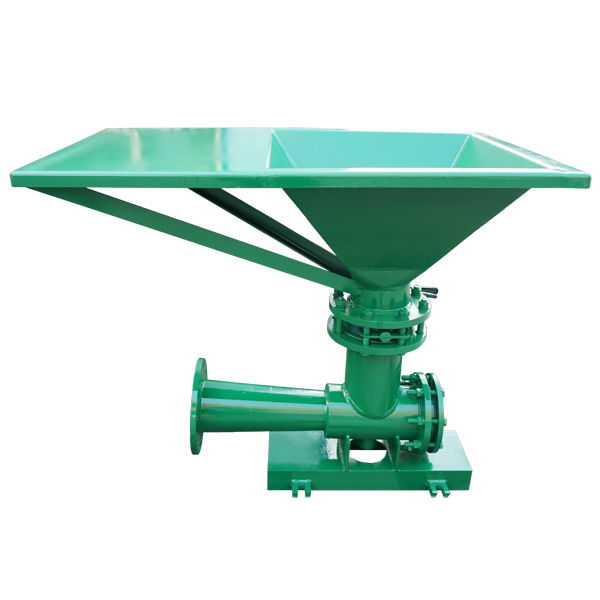
Venturi Mixing Hopper Revolutionizes Mixing Technology in Industrial ApplicationsWith the increasing demand for efficient and effective mixing technology in industrial applications, the introduction of the Venturi Mixing Hopper has been a game-changer in the industry. This innovative solution has been designed to revolutionize the way materials are mixed, offering a more effective and efficient approach to industrial mixing.The Venturi Mixing Hopper, developed by a leading company in the field of industrial equipment manufacturing, has been gaining widespread attention for its ability to significantly improve mixing processes in various industries. This cutting-edge technology has been designed to provide a solution to the challenges faced by industries when it comes to mixing materials effectively and efficiently.The company behind the Venturi Mixing Hopper is known for its commitment to innovation and excellence in the field of industrial equipment manufacturing. With a proven track record of delivering high-quality solutions to industries around the world, the company has built a reputation for pushing the boundaries of what is possible in industrial technology.The Venturi Mixing Hopper is a testament to the company's dedication to innovation and its ability to develop solutions that meet the ever-evolving needs of industries. By combining cutting-edge technology with practical industrial applications, the company has been able to create a product that is not only effective but also efficient and reliable.One of the key features of the Venturi Mixing Hopper is its ability to achieve thorough and uniform mixing of materials, regardless of their properties or characteristics. This has been a significant challenge for industries that rely on effective mixing processes to ensure the quality and consistency of their products. The Venturi Mixing Hopper has been able to address this challenge by utilizing advanced technology that is capable of achieving optimal mixing results.In addition to its exceptional mixing capabilities, the Venturi Mixing Hopper also offers a range of other benefits that make it a valuable investment for industries. Its compact design and user-friendly interface make it easy to operate and maintain, while its robust construction ensures durability and longevity. Furthermore, the Venturi Mixing Hopper is designed to be adaptable to various industrial settings, making it a versatile and flexible solution for different applications.The introduction of the Venturi Mixing Hopper has been met with a positive response from industries that have been struggling with outdated and inefficient mixing technologies. The significant improvements in mixing efficiency and quality that the Venturi Mixing Hopper offers have been a game-changer for these industries, allowing them to optimize their processes and achieve better results.The company behind the Venturi Mixing Hopper has been actively promoting the benefits and advantages of this innovative solution, working closely with industries to demonstrate its capabilities and potential impact. Through various demonstrations and case studies, the company has been able to showcase the significant improvements that the Venturi Mixing Hopper can bring to industrial mixing processes.Moving forward, the company is committed to further developing and enhancing the capabilities of the Venturi Mixing Hopper, as well as exploring new opportunities for its application in different industries. By continuing to innovate and push the boundaries of industrial mixing technology, the company aims to further solidify the position of the Venturi Mixing Hopper as a leading solution for efficient and effective mixing in industrial applications.In conclusion, the introduction of the Venturi Mixing Hopper has been a significant development in the field of industrial mixing technology. With its exceptional capabilities and numerous benefits, this innovative solution has already made a substantial impact on industries that rely on efficient and effective mixing processes. As the company behind the Venturi Mixing Hopper continues to drive innovation and excellence in industrial equipment manufacturing, the future looks promising for the continued success and evolution of this groundbreaking technology.
Desilter Cyclone: Key Features and Advantages Explained
**Innovative Desilter Cyclone Technology Enhances Efficiency in Solid-Liquid Separation**In the ever-evolving field of solid-liquid separation, the latest advancements in desilter cyclone technology are making significant impacts on operational efficiency and environmental sustainability. The innovative desilter cyclone, designed to optimize the separation process, offers substantial improvements compared to traditional methods, making it a key component for industries reliant on effective solids control.The desilter cyclone is a crucial equipment used primarily in drilling operations, wastewater treatment, and other industrial applications that involve the separation of fine solids from liquids. By utilizing centrifugal force, the desilter cyclone efficiently removes suspended particles, reducing the need for chemical additives and lowering overall operational costs.### How Desilter Cyclone Technology WorksThe technology at the heart of the desilter cyclone involves the strategic use of a conical vessel where slurry enters tangentially, creating a vortex. The centrifugal force generated causes the heavier solids to move outward along the cyclone wall, descending to the underflow outlet, while the cleaned liquid moves upward through the central outlet. This process is highly effective in separating solids in the range of 15-44 microns, which are typically challenging to filter through conventional means.### Advantages Over Traditional Solids Control EquipmentIn comparison to conventional shale shakers and hydrocyclones, the desilter cyclone offers enhanced separation efficiency. The higher centrifugal force and improved design lead to better removal rates of fine solids, which is crucial in maintaining fluid properties and preventing issues such as drill string sticking and reservoir damage in oil and gas operations.Moreover, the desilter cyclone contributes to a lower environmental footprint by minimizing waste generation. The reduced chemical use and improved solids capture mean that fewer pollutants are discharged into the environment, aligning with increasingly stringent regulatory requirements.### Applications Across Multiple IndustriesWhile extensively utilized in oil and gas well drilling for maintaining drilling fluid quality, the desilter cyclone's versatility extends to wastewater treatment plants, mining operations, and chemical manufacturing. In wastewater treatment, it serves to clarify water streams by removing suspended solids, improving effluent quality, and supporting water reuse initiatives.Mining companies employ desilter cyclones to separate valuable minerals from waste materials efficiently, enhancing resource recovery rates. Similarly, chemical production units integrate this technology to manage process streams, ensuring product quality and operational stability.### The Company Behind the Innovation[Company Name], a leading player in solids control and environmental protection equipment manufacturing, has been at the forefront of desilter cyclone technology development. With decades of experience in engineering and manufacturing, the company is committed to delivering high-performance, reliable, and cost-effective solutions tailored to meet industry demands.The company’s desilter cyclones are designed with precision-engineered components that ensure durability and consistent performance under harsh operational conditions. Incorporating advanced materials and manufacturing processes, these cyclones stand up to abrasive slurries and high-pressure environments, reducing downtime and maintenance needs.### Customer Success StoriesSeveral clients across different sectors have reported significant improvements after adopting the desilter cyclone technology from [Company Name]. One drilling contractor highlighted a marked reduction in mud losses and drilled solids content, which translated into faster drilling rates and lower costs. Similarly, a municipal wastewater treatment facility noted enhanced clarity in discharged water and reduced chemical consumption, facilitating compliance with environmental standards.### Commitment to Sustainability and Innovation[Company Name] continues to invest in research and development, aiming to refine desilter cyclone designs further and explore integration with digital monitoring systems. This approach is expected to provide real-time performance insights, predictive maintenance capabilities, and optimize operational parameters, adding another layer of efficiency and sustainability to clients’ operations.The company is also focused on sustainability initiatives, ensuring that every new product aligns with global efforts to reduce environmental impacts. Through innovations in energy efficiency and materials recycling, [Company Name] strives to contribute positively toward a greener future.### Future OutlookAs industries face increasing pressure to optimize resource use and minimize environmental impacts, technologies like the desilter cyclone will become even more critical. Its ability to reliably and efficiently separate fine solids from liquids ensures operational continuity, cost savings, and environmental compliance.With continued innovation and customer-centric solutions, [Company Name] is positioned to meet the growing demand for advanced solids control technologies worldwide. The company’s dedication to quality and innovation underscores their role as a trusted partner in improving operational efficiency and advancing environmental stewardship.---**About [Company Name]**[Company Name] is a global leader specializing in solids control equipment and environmental protection solutions. Founded on a commitment to quality and innovation, the company serves a diverse range of industries including oil and gas, mining, wastewater treatment, and chemical processing. With a comprehensive product portfolio and an emphasis on research and development, [Company Name] delivers reliable, efficient, and sustainable products designed to meet the complex challenges of modern industrial operations.---The advancement and widespread adoption of desilter cyclone technology reflect the ongoing drive toward more effective, safer, and environmentally responsible industrial practices. As [Company Name] continues to innovate and support its clients, the future of solids control looks promising—paving the way for enhanced performance and sustainability in multiple sectors.---[Note: Replace placeholders such as [Company Name] with the actual company details as appropriate.]